

Inside the Factory: The 5-Step Quality Testing Process for Car Inverters
- Introduction: Why Uncompromising Quality Control Matters for Car Inverters
- Pre-Production: Raw Material Inspection and Component Selection
- Step 1: Initial Assembly Inspection & Waveform Distortion Analysis
- Step 2: Electrical Safety Testing & Smart Protection Validation
- Step 3: Extreme Thermal Management & Full-Load Burn-in Testing
- Step 4: Environmental Adaptability, Vibration, and Shock Testing
- Step 5: Final QA Inspection & Global Safety Certification
- Troubleshooting and Debugging During the QC Process
- The Business Impact: Validating Long-Term Reliability and Lowering RMA
- Conclusion: Secure Your Supply Chain with CSINVERTER
- Frequently Asked Questions (FAQs)
Introduction: Why Uncompromising Quality Control Matters for Car Inverters
In the highly competitive global automotive electronics market, uncompromised quality control is the ultimate baseline for long-term B2B success. A car inverter serves as the critical bridge between a vehicle’s sensitive 12V/24V battery and high-voltage AC appliances. For global distributors, wholesale buyers, and OEM brands, transparent and rigorous factory-level quality assurance is not just about meeting basic safety standards; it is the core defense against catastrophic fire hazards, brand-damaging public relations crises, and depleted profit margins. When electronic components fail in the field, the resulting damage can destroy customer trust instantly. This is why leading manufacturers prioritize a systematic testing approach. By implementing an exhaustive 5-step quality testing process, factories ensure that every unit leaving the assembly line is fortified against extreme mechanical and electrical stress. This insider guide reveals how meticulous manufacturing protocols safeguard both the end-user's safety and the distributor's financial bottom line, proving that true reliability begins long before the product is ever boxed.
Pre-Production: Raw Material Inspection and Component Selection
Exceptional product reliability always begins at the supply chain source. Long before the official 5-step testing process commences, rigorous pre-production material inspection is mandatory. A premium car inverter is only as durable as its foundational components. Factory technicians perform strict incoming quality control (IQC) on all raw materials, including pure copper transformers, high-temperature electrolytic capacitors, and top-tier MOSFETs. By utilizing advanced electrical testing jigs, engineers sample-test these components for precise tolerance levels, rejecting any batches that exhibit high equivalent series resistance (ESR) or thermal instability. This aggressive upstream filtering prevents systemic manufacturing defects from ever reaching the assembly line. Whether building a complex pure sine wave unit or a highly efficient modified wave model, selecting premium internal hardware guarantees a longer lifespan, higher conversion efficiency, and sustained electrical stability. This proactive component screening is the critical first step in building power solutions that distributors can sell with absolute confidence.
Step 1: Initial Assembly Inspection & Waveform Distortion Analysis
The first official step in the quality control protocol takes place immediately following the initial PCBA (Printed Circuit Board Assembly). During this phase, engineers conduct comprehensive visual inspections and functional tests to identify any soldering anomalies or incorrect component placements. More importantly, this step involves critical waveform distortion analysis. Using high-precision oscilloscopes, technicians measure the Total Harmonic Distortion (THD) of the output power. This is essential not only for pure sine wave models but also when calibrating a highly efficient 200W Modified Sine Wave Car Power Inverter, ensuring the stepped waveform remains perfectly stable for standard electronics without generating excessive electrical noise. By validating the output wave purity at this early stage, the factory guarantees that the inverter will deliver smooth, reliable power, completely avoiding the risk of damaging the customer's sensitive laptops, portable chargers, or automotive accessories during daily commutes.

Step 2: Electrical Safety Testing & Smart Protection Validation
Electrical safety is the non-negotiable cornerstone of automotive power conversion. Step two pushes the inverter’s smart protection mechanisms to their absolute limits through aggressive electrical stress testing. Engineers intentionally trigger worst-case scenarios—such as short circuits, severe overloads, and reverse polarity connections—to validate the microprocessor's emergency response times. For versatile models like a 150W Dual Input Modified Sine Wave Car Inverter, testers must rigorously verify that the low-voltage disconnect (LVD) and over-voltage protection (OVP) activate flawlessly across both input methods, instantly cutting off power to prevent draining or irreparably damaging the vehicle’s alternator and battery. This intensive safety validation ensures that the smart circuitry acts as a fail-safe firewall. By confirming that the inverter can autonomously protect itself and the vehicle from sudden electrical surges or user errors, the factory delivers a foolproof product that is inherently safe for everyday consumers.
Step 3: Extreme Thermal Management & Full-Load Burn-in Testing
Heat is the primary enemy of electronic longevity, making thermal management the most critical hurdle in manufacturing. Step three involves the grueling full-load burn-in test. Every assembled unit is placed inside a specialized, high-temperature environmental chamber and forced to operate at 100% capacity for several consecutive hours. This intense thermal stress test is particularly crucial for highly compact devices like a 300W Mini Car Power Inverter, where internal space is extremely limited and heat dissipation must be perfectly optimized. Engineers monitor the effectiveness of the aluminum heat sinks and the automated cooling fans using thermal imaging cameras. If any internal component exceeds safe thermal thresholds, the unit is immediately flagged. This rigorous burn-in process effectively eliminates early-stage component mortality (the "infant failure" phase), guaranteeing that the inverter will not overheat, melt, or pose a fire hazard during long road trips or heavy continuous usage.

Step 4: Environmental Adaptability, Vibration, and Shock Testing
Car inverters are subjected to harsh operational environments that standard home electronics never experience. Step four ensures maximum physical durability through rigorous environmental adaptability and vibration testing. Because these devices are frequently installed in off-road vehicles, commercial trucks, and RVs, they must endure relentless mechanical shocks. Inside the factory, completed units are securely strapped to multi-frequency vibration tables that simulate thousands of miles of severe, bumpy road conditions. Engineers then inspect the internal PCB to confirm that the automotive-grade adhesive dispensing (potting compound) has successfully prevented components from vibrating loose and that no solder joints have cracked. Furthermore, testing in specialized humidity and temperature chambers verifies that the inverters can seamlessly cold-start in freezing arctic climates and resist internal condensation in tropical environments. This guarantees that the hardware remains physically intact and fully operational, regardless of the geographic destination or harsh terrain.

Step 5: Final QA Inspection & Global Safety Certification
The final barrier before any product leaves the factory is the comprehensive Quality Assurance (QA) inspection and compliance verification. Step five involves a meticulous cosmetic and functional review of the finished, fully-cased inverter. Every button, USB port, and AC socket is manually tested for tactile integrity and secure fitment. Additionally, the units undergo a critical high-voltage isolation test (Hi-pot test) to ensure complete electrical separation between the high-voltage AC output and the low-voltage DC chassis, eliminating any risk of user electrocution. Simultaneously, compliance engineers verify that the product's performance strictly aligns with international regulatory standards such as CE, FCC, RoHS, or ETL. By ensuring all safety certifications and labeling are perfectly accurate, the manufacturer guarantees seamless global customs clearance and fully legal retail distribution, empowering B2B clients to confidently sell their products in North America, Europe, and emerging global markets.
Troubleshooting and Debugging During the QC Process
A world-class manufacturing facility does not merely discard failed units; it utilizes them to constantly refine the production line. When an inverter fails any of the rigorous five-step tests—whether due to minor voltage fluctuations, high-frequency coil whine, or an unresponsive cooling fan—it is immediately intercepted and sent to the specialized troubleshooting and debugging team. Here, senior electronic engineers dissect the flagged unit to identify the exact root cause of the anomaly. Whether it requires a minor firmware adjustment to the microcontroller or a slight calibration in the soldering temperature profile, the debugging team resolves the issue at the source. This rapid feedback loop guarantees that systemic technical flaws never make it into the packaging boxes. By isolating and fixing problems on the factory floor, the manufacturer ensures that the final batch delivered to the distributor is practically flawless, upholding the highest standards of production excellence.
The Business Impact: Validating Long-Term Reliability and Lowering RMA
For B2B distributors and wholesale buyers, rigorous factory testing is not just a technical necessity; it is a profound financial advantage. The direct business impact of these five unyielding quality control steps is a dramatic reduction in the Return Merchandise Authorization (RMA) rate. Handling cross-border returns, paying for international warranty shipping, and refunding angry customers can rapidly obliterate a distributor's profit margins. By enforcing 100% full-load burn-in testing and strict vibration analysis, the factory absorbs the cost of failure locally, ensuring that only highly reliable, long-lasting hardware reaches the overseas market. This translates directly into minimized maintenance costs, protected retail margins, and a stellar brand reputation among end-users. Ultimately, partnering with a manufacturer that prioritizes long-term reliability transforms the car inverter from a high-liability electronic accessory into a highly profitable, worry-free cornerstone of your automotive parts catalog.
Conclusion: Secure Your Supply Chain with CSINVERTER
Eliminating product failure requires more than basic testing; it demands a manufacturing partner committed to absolute reliability. CSINVERTER provides uncompromising quality control through our rigorous 5-step testing protocol. By combining deep OEM/ODM customization with full-lifecycle technical support, we ensure your global distribution network operates flawlessly. Partner with CSINVERTER today to lower your RMA rates, protect your brand reputation, and deliver world-class car inverters to your market.
Frequently Asked Questions (FAQs)
How does CSINVERTER select and inspect raw materials for car inverters?
We implement rigorous Incoming Quality Control (IQC), testing critical components like MOSFETs, capacitors, and transformers for precise electrical tolerances before assembly. This prevents low-quality materials from entering the production line and ensures foundational durability.
What exactly is the "Burn-in Test" and why is it critical for durability?
The Burn-in Test forces the fully assembled inverter to run at 100% maximum capacity inside a high-temperature chamber for several hours. This exposes and eliminates weak components that might fail early in their lifespan, ensuring ultimate thermal stability.
What environmental and vibration conditions can the inverters withstand?
Using high-frequency vibration tables and climate chambers, we simulate extreme off-road bumping, arctic freezing, and tropical humidity. Combined with automotive-grade internal potting adhesives, our inverters easily survive the harshest physical driving conditions.
How are the smart protection features (like short-circuit and battery drain) tested?
Engineers artificially induce severe overloads, short circuits, and extreme voltage drops to verify that the microchip instantly triggers features like the Low Voltage Disconnect (LVD), guaranteeing the vehicle's battery is never depleted or damaged.
How does a strict QC process actually save me money as a distributor?
By intercepting defective units at the factory, we drastically lower your Return Merchandise Authorization (RMA) rate. This eliminates the high costs of international return shipping, local repairs, and lost retail margins, directly maximizing your profitability.
Does CSINVERTER provide international safety certifications for global markets?
Yes. During final inspection, our compliance team ensures each unit passes strict high-voltage isolation (Hi-pot) testing and meets all required international standards, including CE, FCC, RoHS, and ETL, facilitating smooth global customs clearance.
Can the QC testing process be customized for specific OEM/ODM projects?
Absolutely. If your target market involves unique environments (like marine applications with high salt-fog), CSINVERTER's engineering team can integrate specialized anti-corrosion and extreme temperature testing protocols directly into your custom manufacturing process.
How does CSINVERTER handle full lifecycle technical support after the sale?
Beyond delivering pristine hardware, we provide extensive aftermarket support, including technical troubleshooting guides, a reliable supply of spare parts, and comprehensive warranty backing to ensure your distribution business operates without disruption.


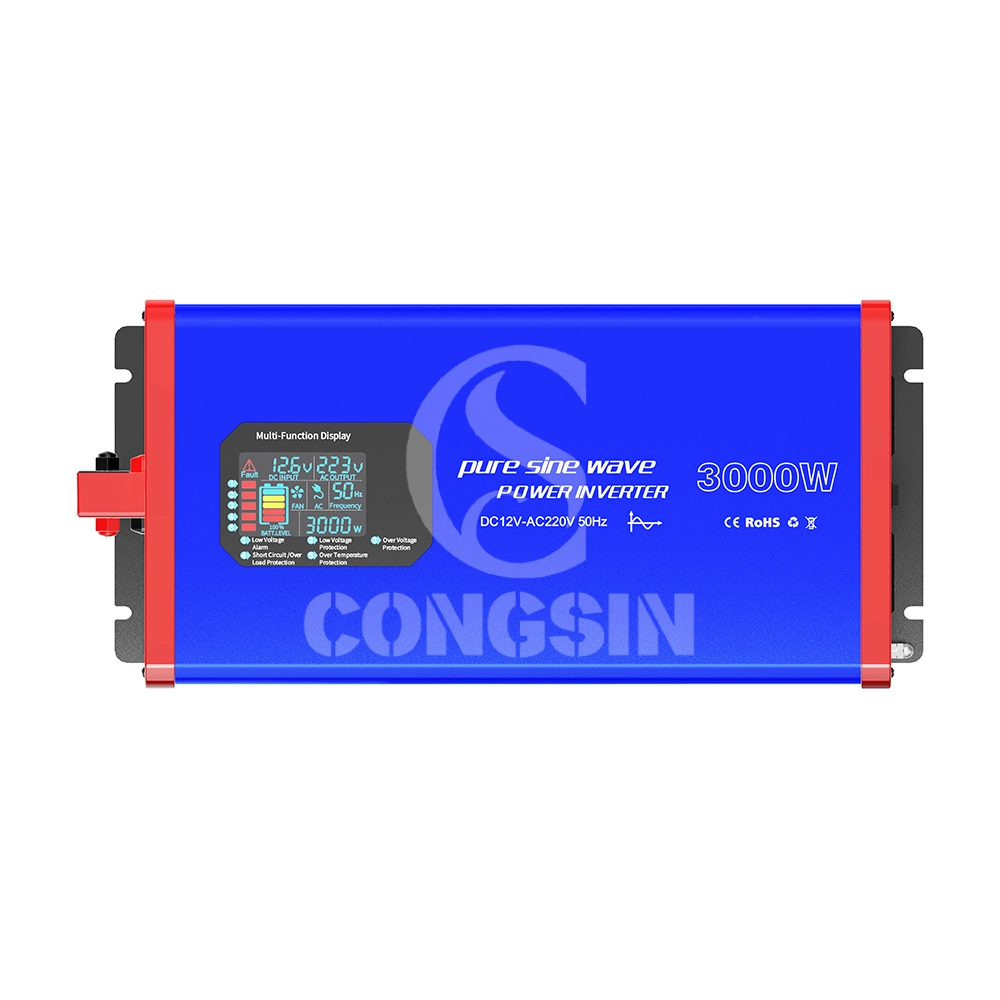
This 3000W full-power pure sine wave inverter (Model: CS3000PSW) adopts pure sine wave output technology (waveform distortion rate <2%), and the output power is highly consistent with mains power quality. It can safely drive high-power precision loads such as air conditioners, refrigerators, medical instruments, and small industrial equipment, avoiding equipment malfunctions or shortened service life caused by unstable waveforms. The device supports DC 12V input (compatible with 10.5V-14.8V wide voltage), continuously outputs 3000W full power, and has a peak power of 6000W, easily coping with the instantaneous startup impact of high-power devices; it is equipped with 4 AC universal sockets (max current 16A) + 2 USB 3.0 fast-charging ports (22.5W per port) to meet the simultaneous power supply needs of multiple devices. Built-in six-fold safety protection (overload, overvoltage, undervoltage, short circuit, overtemperature, reverse connection), combined with dual intelligent silent cooling fans (noise ≤45dB), it achieves the triple advantages of "high power + high safety + low noise," suitable for home emergency, outdoor engineering, vehicle-mounted power supply, small industrial scenarios and other fields.
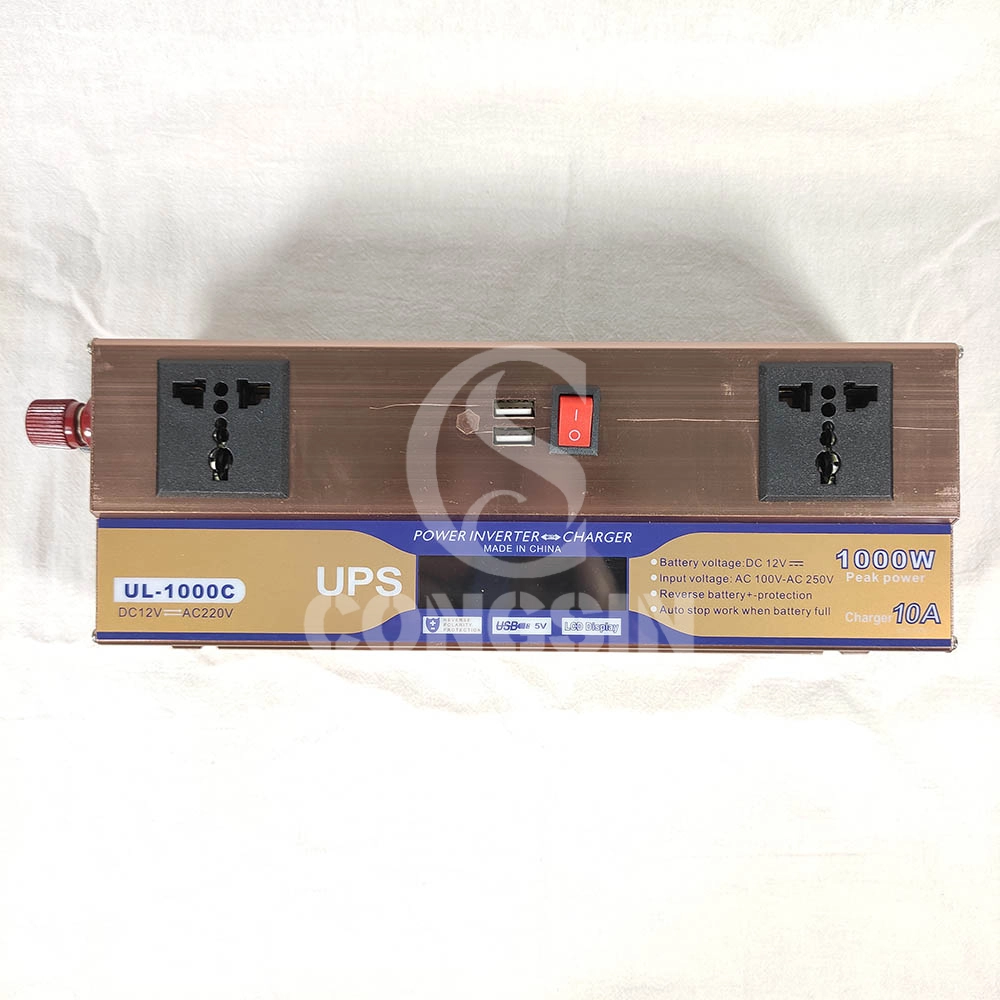
This 1000W modified sine wave inverter has UPS charging function, with DC12V input and AC220V output, and 600W rated power. Equipped with dual universal sockets, two USB ports, an LCD display, and a battery clip, it is professionally designed and has stable performance. It can provide stable AC power conversion and UPS emergency power supply for computers, small home appliances, electronic devices, etc. in home emergency, office, outdoor and other scenarios, meeting the needs of simultaneous power supply and emergency power supply for multiple devices.

This 1500W pure sine wave inverter converts DC 12V to AC 220V power, with a rated power of 1500W and a peak power of 3000W. Equipped with dual fans, LCD display, QC3.0 and PD Type-C fast charging ports, and remote control capability for stable and intelligent power output.

Our CS2000BIG 2000W modified sine wave inverter is a high-power power conversion device that converts DC 12V from batteries into AC 220V electricity. It is designed for heavy-duty use, featuring 2 AC sockets to power multiple high-power devices simultaneously, 2 cooling fans for efficient heat dissipation, and battery terminal wire for stable connection. With its robust construction and large capacity, it is an ideal solution for powering tools, appliances, and equipment in various scenarios, from industrial use to home emergencies.
Get in Touch with Our Team
You can also communicate with us directly through our online contact form. Please fill in the following information, and our team will contact you as soon as possible after receiving your message.
CONGSIN is a trusted OEM factory for power inverters, solar charge controllers, and DC converters. Reliable solutions for global B2B buyers.
 High Quality
 7/24 Service
 Guaranteed Warranty
© 2025 Congsin. All Rights Reserved.
 WeChat
 Scan QR Code
sin cong
teaimei10
Whatsapp: +8618028086791
Scan QR Code